Products >> Railway Wheelsets >>


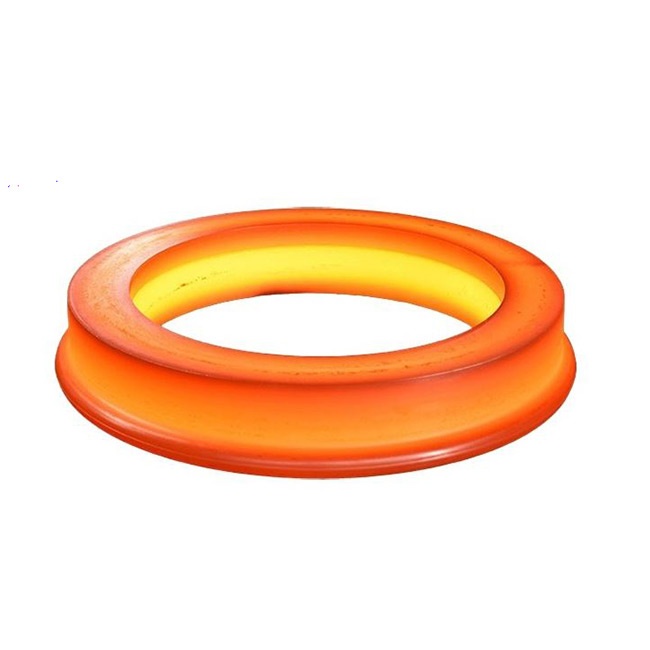


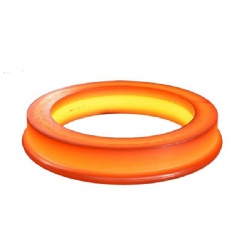
AAR Standard High-Durability Steel Railway Wheel Tyres
- Product No.:2026453378
- Price:negotiation
- Material:M201
- Standard:AAR
- mould charge:yes
- Production time:75
- weight:120
- Package:Wooden Box
Forged Railway Tyre of Railway Locomotive wheel
1. High Fatigue Resistance — Forged from LG61/B6E alloy steel, suitable for 200km/h operation. Precision Profile Machining — CNC ensures smooth wheel-rail contact, reducing wear. Full Traceability — Heat number stamped, MTC EN 10204 3.1 available. Low Noise Design — For metro and LRV resilient wheel applications
 |
 |
AAR Standard High-Durability Steel Railway Wheel Tyres - supplied by Suzhou Guanyi Machinery
KEY PRODUCT ADVANTAGES
1. Electric locomotives. Diesel locomotives. Steam locomotives. Industrial & Mining combination wheels. Resilient wheel core replacement

APPLICATIONS
Product Matrix
| Product Type | Forged Railway Tyre |
|---|---|
| Outer Diameter | 600–1750 mm (Catalog P20) |
| Inner Diameter | 450–780 mm (Matched to wheel core) |
| Material | LG61 / B6E / B3 / B4N (Catalog P21) |
| Hardness | HB 240–280 (TB/T1882 Standard) |
| Standards | TB/T1882-2001 / BS5892PART4 / UIC810-1 |
| Design Parameters | Axle Load ≤26t / Speed ≤200km/h (Catalog P21) |
| Process | Forging + Heat Treatment + CNC Machining |
High-strength forged railway tyres for resilient wheels and combination wheels. Outer diameter 600-1750mm, material grades LG61/B6E/B3 per TB/T1882, BS5892PART4, UIC810-1. Applied in electric locomotives, diesel locomotives, and steam locomotives.
From ingot to finished tyre
A railway tyre is a ring that has to hold its shape through millions of wheel revolutions, so the process matters as much as the chemistry. Billets are cut, heated and upset, then pierced and rolled to a ring blank with the grain flow running circumferentially, which is the direction that resists the hoop stress of a shrinking fit. After rolling, the tyre is heat treated to refine the structure and to reach the hardness range in the table above, then machined on a CNC profile lathe to the final tread contour and the mounting bore.
- Forged and rolled ring, with circumferential grain flow
- Controlled heat treatment, hardness checked on each batch
- CNC profile machining of tread, flange and bore
- Ultrasonic inspection of the ring for internal defects
- Dimensional check of bore, width and profile against the drawing
Fitting to the wheel centre
The tyre is fitted by shrinking: the tyre is heated, the wheel centre is inserted, and the assembly is allowed to cool so that the interference holds the ring in place. Fit tolerances and the heating temperature have to be respected, because an under-tight tyre will creep on the centre and an over-tight one can crack at the bore. We machine the bore to the interference specified for the customer's wheel centre, and mark the tyre so that the matching centre is identifiable at the press.
Service, wear and re-profiling
Tread wear is the normal life limit. The profile is inspected for flange thickness, flange height and tread hollowing, and the tyre is re-profiled on a wheel lathe while there is still material above the condemning limit. Because the hardness range is held through the depth of the tread, re-profiling does not expose a soft layer. Tyres that have reached the limit, or that show shelling or thermal cracks, are scrapped rather than built up.
Ordering information
Give us the outer diameter, the inner diameter and the tread profile drawing, together with the axle load and the maximum operating speed. We confirm the material grade, the hardness range and the standard before production. Standard lead time is about 75 days, packed in wooden cases with the bore protected against corrosion for sea freight.
Related Products

Price: negotiation

Price: negotiation

Price: negotiation

Price: negotiation
Price: negotiation

Price: negotiation
Products Category
Contact Us
Name: Meiya
Tel: +86 15151598778
E-mail: meiya@guarail.com
WeChat: +86 15151598778
Whatsapp: +86 15151598778
Add: B1608 room Building 5 of Tainhe Huayuan ,YangJian Twon,Suzhou city ,Jiangsu ,China

 WhatsApp
 Mail inquiry